


Stop Wasting Energy:
Optimize Industrial Steam Boiler Performance via Online Analytics
Fluctuating production schedules require modern steam systems to react dynamically. Yet, in many industrial plants, water treatment remains critically rigid. Operating teams often set chemical dosing rates and deaerator venting to permanent maximum loads to guarantee safety during peak demands.
The hidden cost? Massive thermal energy penalties, thousands of cubic meters of wasted process water, and excessive chemical consumption during low-load periods.
Transitioning to automated, demand-initiated water conditioning safeguards your steam generation infrastructure while reducing overall operating costs by up to 10%. By continuously tracking your exact water parameters, you eliminate manual testing loops, reduce fuel usage, and cut Scope 1 carbon emissions.
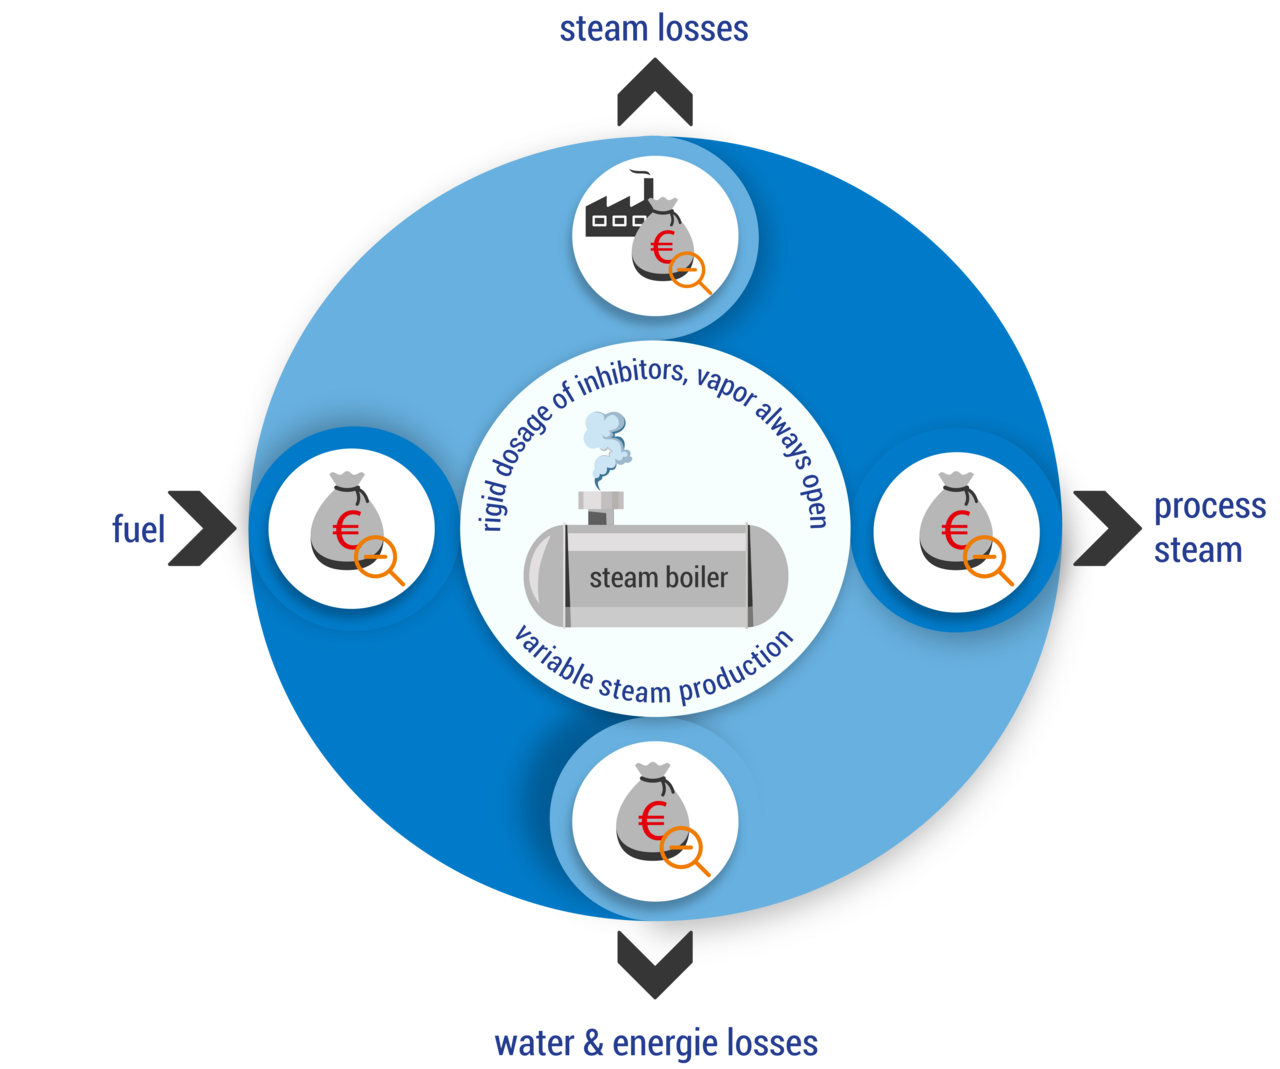
Rigid dosing of inhibitors in the steam boiler costs time, money, water and energy
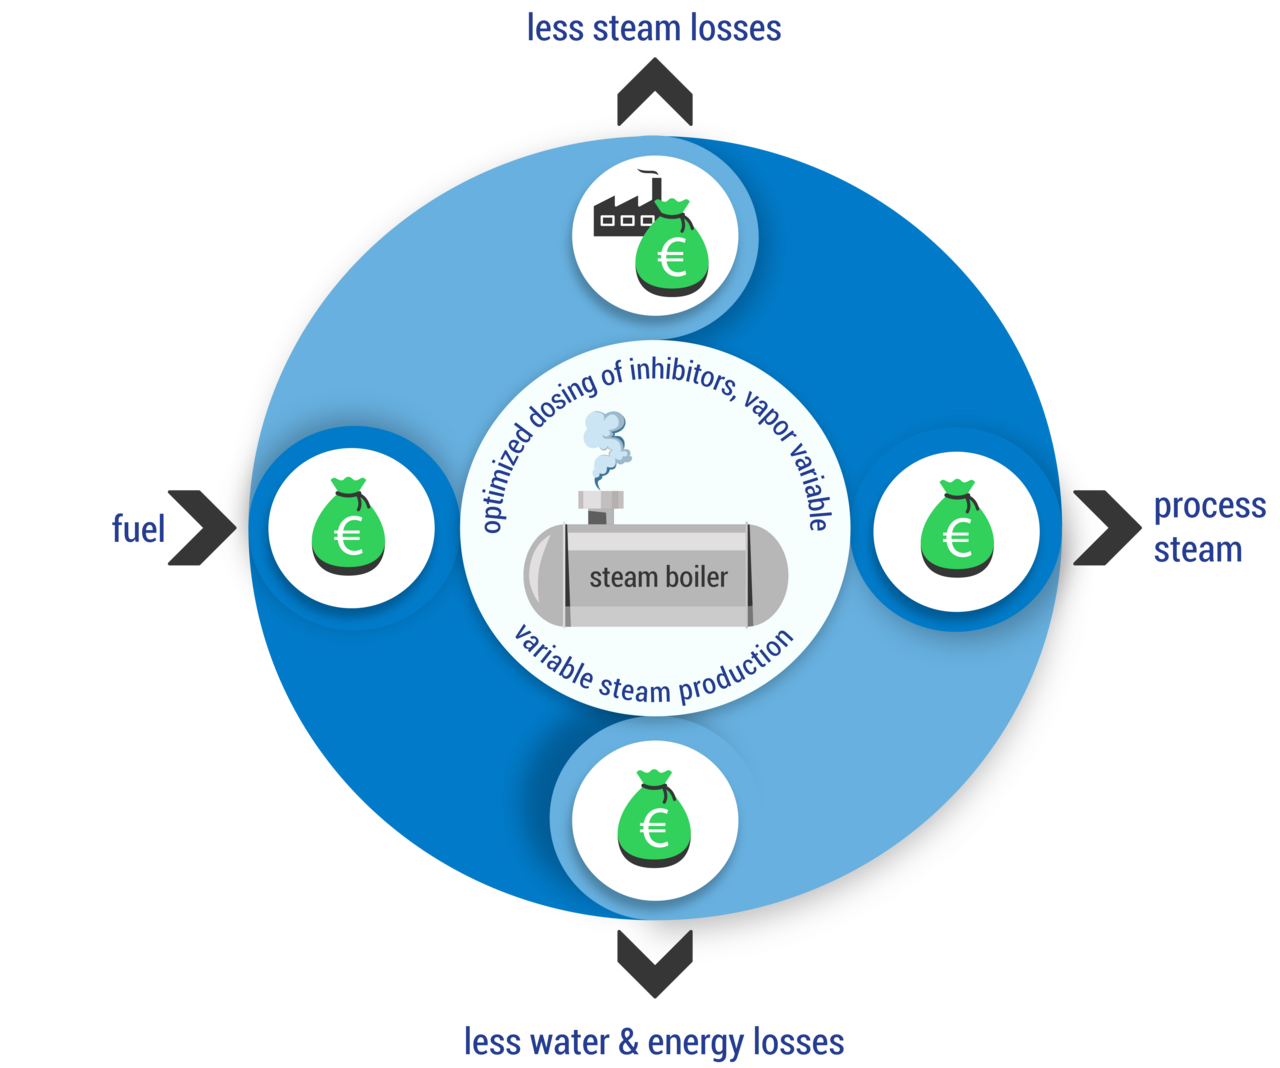
Optimized dosing of inhibitors leads to savings in water, energy and service
Minimize Exhaust Vapor Losses: Intelligent Control of the Deaerator Vent Valve
To guarantee reliable thermal deaeration and prevent pitting corrosion, the vent valve of a feedwater tank typically stays open. Without continuous, online data, precious steam escapes into the atmosphere completely unnoticed.
Real-time dissolved oxygen (DO) monitoring completely changes this equation. When our sensors verify that the feedwater is entirely oxygen-free, your control system can safely throttle or close the exhaust vapor valve.
How Online Analytics Saves You Money Here:
- Zero Steam Waste: Eliminates unnecessary thermal and water mass losses during low-load operation.
- Prevents Chemical Over-Salting: Automates oxygen scavenger dosing, avoiding excessive sodium sulfite accumulation (up to 10 mg/l).
- Optimized Boiler Blowdown: Lower chemical input means a lower salt load, which significantly reduces the required blowdown volume and retains precious boiler heat.
The OFS Solution: Our automated OFS FWO-Control integrates seamlessly with your vent hardware to transform manual tanks into self-optimizing thermal units.
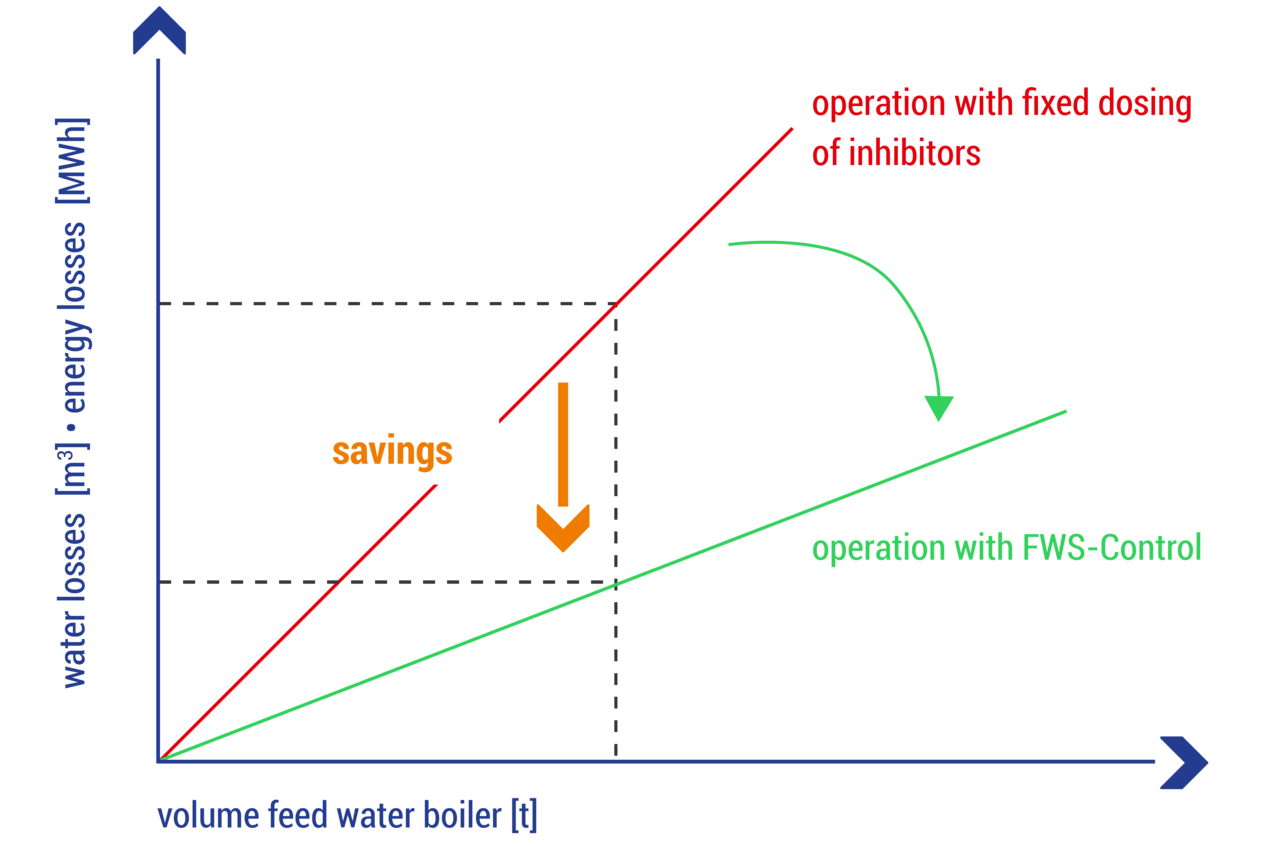
Saving water, energy and carbon dioxide through online measurement of feed water with vapor control
Volume of feed water boiler
Overpressure in the feed water boiler
Condensate content to the feed water
Effect per year
Water saving
Energy saving
CO2 saving with fuel heating oil
CO2 saving with fuel natural gas
Prevent Boiler Scale and Corrosion with Demand-Triggered Inhibitor Dosing
Maintaining a slightly alkaline pH value between 9.0 and 10.0 in the feedwater circuit is mandatory to fulfill legal guidelines and prevent corrosion. However, blind over-dosing during low steam production cycles spikes your chemical bill and can increase water and energy losses up to tenfold.
Automated online monitoring of pH, residual oxygen, and specific electrical conductivity tracks the exact Cycles of Concentration (CoC) inside the boiler drum. Chemical dosing pumps respond instantly to actual demand rather than fixed timers.
Operational Benefits at a Glance:
- Controlled Conductivity: Prevents scale deposits on heat exchanger surfaces, securing optimal heat transfer.
- Automatic Electronic Log: Replaces error-prone manual paper logs with continuous, legally compliant data storage.
- Reduced Maintenance Effort: Real-time diagnostics trigger immediate alarms before critical system failures or short-cycling occur.
The OFS Solution: The OFS HWA Analyzer combines all three critical parameters into a single, chemical-free, low-maintenance control unit for automated plant balancing.
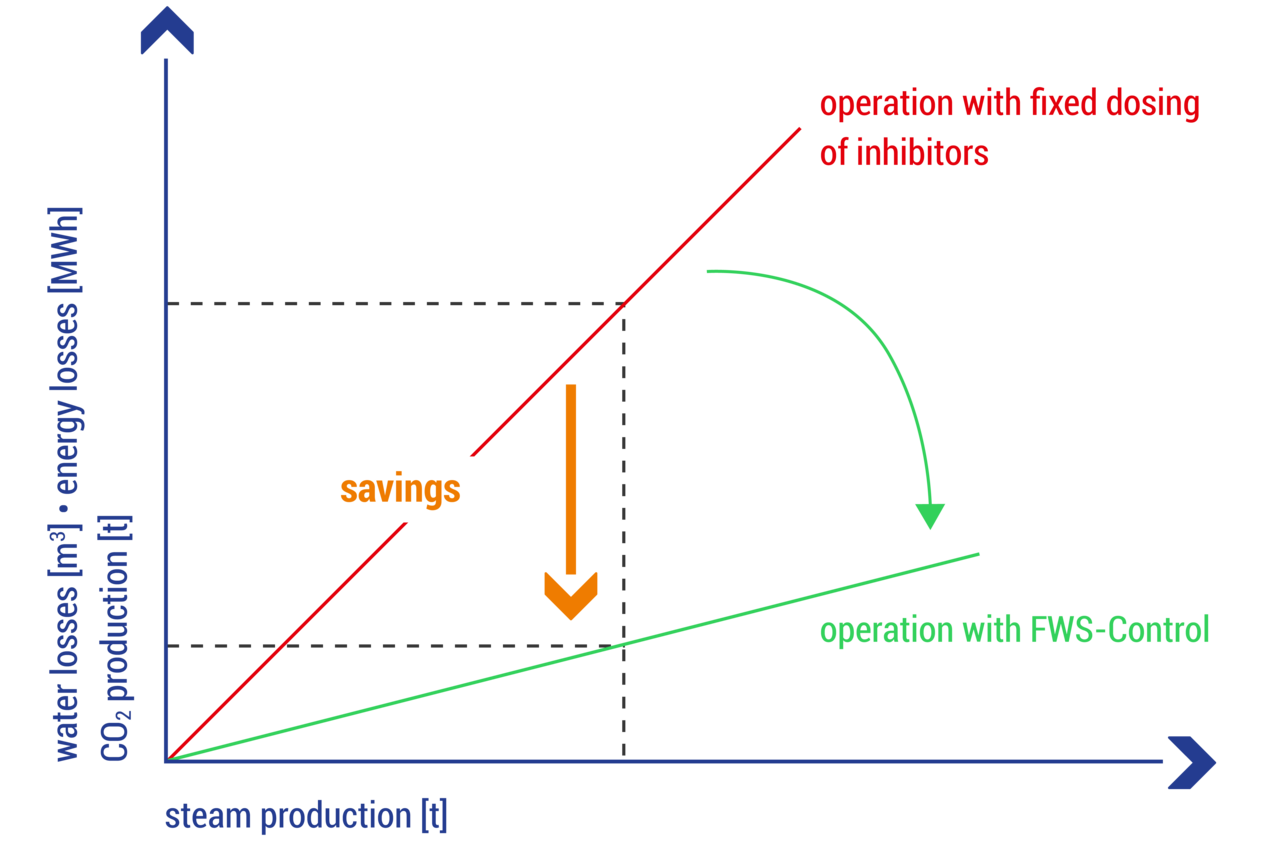
Saving water, energy and carbon dioxide by online measurement with quality control of inhibitors
Pressure rating of steam boiler
Blowdown conductivity of steam boiler
Ø conductance of make-up water
Ø pH value feed water
Steam production per year
Effect per year
Water saving
Energy saving
CO2 saving with fuel heating oil
CO2 saving with fuel natural gas
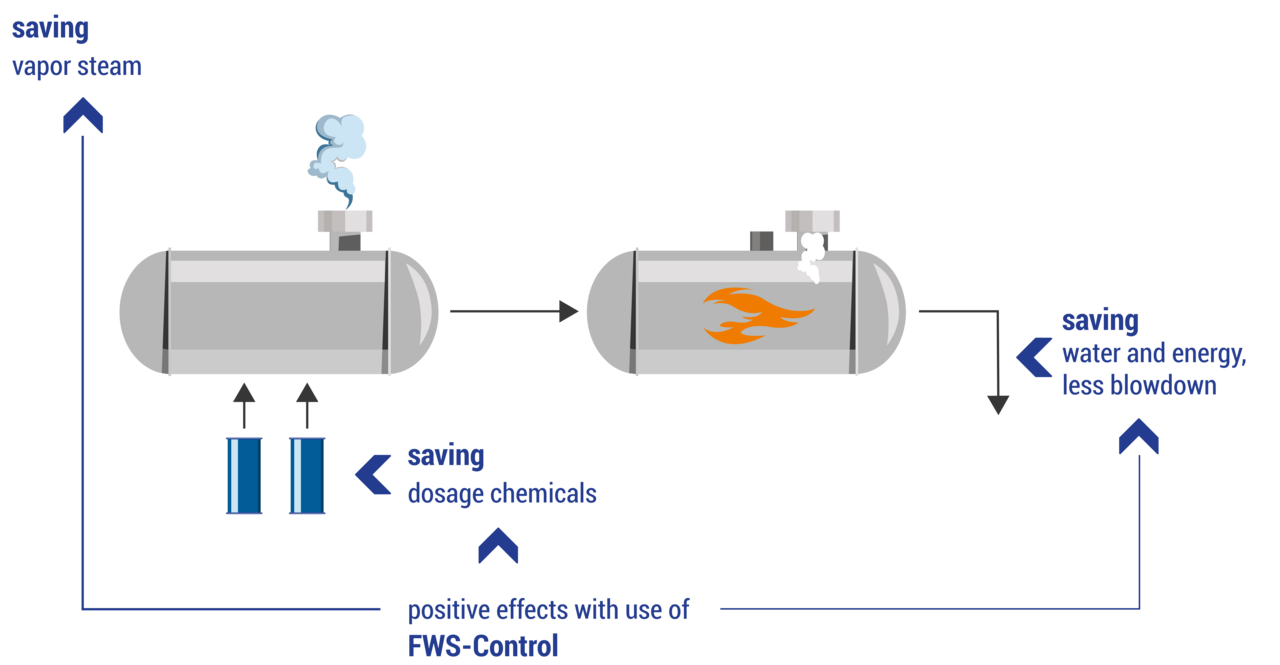
Total water, energy and carbon dioxide savings by online measurement with quality control of inhibitors and vapor valve
Total effect per year
Water saving
Energy saving
CO2 saving with fuel heating oil
CO2 saving with fuel natural gas
Total water and energy savings based on the total annual amount of steam production
Total effect per year (per ton of steam)
Water saving
Energy saving
The results from the tables will differ in practice, since not all concrete conditions can be taken into account in this form. These results should be your first decision-making aid for optimizing and increasing the efficiency of your steam boiler system.
Control and dosing of feed water and steam boiler
Ready to Reduce Your Plant’s Thermal Bill? Let’s Optimize Your Boiler
Every industrial steam system has unique operational parameters. Contact our engineering specialists today for a technical consultation. Let us show you how easily our compact, reagent-free online analyzers integrate into your existing control loops to maximize process safety and cost-efficiency with HWA Analyzer